If you’ve ever worked with a hydraulic surface grinder, you know these machines are the workhorses of precision machining—they grind flat, smooth surfaces with tight tolerances that make aerospace parts, mold components, and automotive gear heads fit perfectly. But here’s the thing: a neglected grinder loses its edge, produces inconsistent finishes, and can even break down mid-job, costing you time and money. As a hydraulic surface grinder supplier, I’ve walked hundreds of customers through maintenance routines, and cleaning is the foundation of keeping these machines running like new. Let’s break this down step by step, with the kind of practical advice I tell every buyer when they pick up their new grinder. Hydraulic Surface Grinder
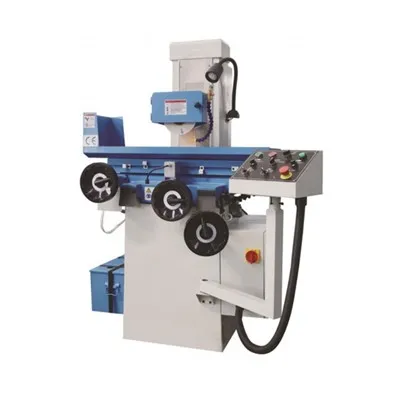
First, why is cleaning a hydraulic surface grinder so different from wiping down a drill press or a lathe? Unlike smaller tools, these machines have a hydraulic system at their core—oil that powers the ram, feeds the workpiece, and maintains that smooth, controlled movement. Any debris, swarf, or coolant buildup doesn’t just sit on the surface; it gets dragged into tiny valves, seals, and hydraulic lines, causing clogs that make the ram stick or jerks during a cut. I saw this first-hand with a local mold shop last year: they skipped monthly cleaning, and their hydraulic surface grinder’s table seized mid-run on a set of plastic injection molds, costing them a $12,000 rush job and three days of downtime. That’s the risk we avoid when we clean the right way.
Let’s start with prep work. You don’t want to dive into wiping parts without setting yourself up for safety and efficiency. First, unplug the machine—never skip this step, even if you’re only cleaning the table. The last thing you want is the hydraulic ram engaging unexpectedly. Next, drain the old coolant from the sump. I tell customers to do this when the machine is still warm, because warm coolant flows more easily and carries more swarf with it. If the coolant is really dirty, you can strain it through a fine mesh filter to reuse it, but most of the time, it’s time to replace it. Then, gather your supplies: a stiff nylon brush (brass is too soft, steel can scratch precision surfaces), a lint-free microfiber cloth, a hydraulic-safe degreaser (not the oven cleaner under your sink—harsh chemicals eat at hydraulic seals), rubber gloves, safety goggles, and a small magnetic tool for picking up tiny metal shavings from hard-to-reach spots. Skip the pressure washer here; the high pressure can push debris into hydraulic seals or etch the machine’s cast iron surface, which ruins the flatness we work so hard to maintain.
Now, let’s go through each component, because cleaning isn’t just about the main table. The table is the most visible, and the most critical. Most surface grinder tables are magnetic—permanent magnets or electromagnetic—and swarf sticks to them like glue. A lot of people use a steel scraper to get it off, but I don’t recommend that: even a dull scraper can leave tiny scratches on the table that will show up on your workpiece. Instead, use that magnetic tool first to lift any loose shavings, then spray a small amount of hydraulic degreaser on the table, let it sit for 30 seconds to break down coolant residue and oil, then gently scrub with the nylon brush, focusing around the T-slots where swarf loves to hide. The T-slots are especially important because that’s where you clamp down workpieces—debris there can make your workpiece sit unevenly, leading to out-of-flat parts. Once you’re done scrubbing, wipe the table dry with the microfiber cloth, then run a clean, dry cloth along the surface to make sure you didn’t miss any tiny particles. If you have an electromagnetic table, double-check the corners—they’re often the last place debris gets wiped, and that’s where uneven magnetism causes workpiece shift.
Next, the hydraulic system’s external components, because that’s where the visible wear shows. The hydraulic ram, the part that moves the grinding wheel head up and down, has a smooth cast iron surface that needs to stay free of grime. Wipe it down with a degreaser-soaked cloth, but don’t use too much liquid—you don’t want fluid seeping into the ram’s seals, which can cause leaks. Then, move the ram through its full range of motion as you clean: this pushes any trapped debris out of the seal gaps. If you notice any oil spots on the floor around the ram or the hydraulic tank, take note of them—those can be signs of worn seals, which we can replace during your next service. The hydraulic tank itself: you don’t need to drain it every time, but once a quarter, wipe the outside down, and if you see sediment at the bottom, a small siphon can pull that out without draining all the oil. Never top off the hydraulic oil with any kind of motor oil—always use the grade recommended by your grinder’s manual, a tip I give every customer when they get a new machine from our team.
Then, the grinding wheel and the wheel guard—two parts that directly affect finish quality. The wheel guard is where swarf and coolant spray collect, so it’s easy to skip, but it’s a mistake. Clamp a rag around the guard’s opening to catch debris, then use the nylon brush to scrub inside the guard—don’t stick your hands in while the machine is plugged in, obviously. For the grinding wheel itself, you’ll need to dress it before and after cleaning, right? Wait—some people clean the wheel first, but I find that if you dress the wheel before cleaning, the dressing removes any glaze that’s built up, and then cleaning removes the leftover dressing compound and swarf. To dress the wheel, use a diamond dresser, hold it steady, and move it across the wheel face a few times, then run the machine for 10 seconds to spin the wheel and blow out loose particles. Then, use a stiff brush to gently brush the wheel’s face from center to edge (never scrub back and forth, that can damage the wheel’s bond) to remove any remaining swarf. If the wheel is really clogged, you can use a small amount of coolant on the brush, but don’t soak the wheel—excess moisture can cause the wheel to crack when it heats up during grinding.
Don’t forget the other easy-to-miss spots: the way around the grinding head’s base, the control panel, and the workpiece rest. The control panel might have grease from your hands, so wipe it with a damp (not wet) cloth—never spray degreaser directly on controls, that can seep into the buttons and cause them to stick. The workpiece rest, the small bar that sits next to the wheel to support your part, should be removed occasionally, scrubbed, and checked for wear—if it’s got a groove from the wheel, it’s time to replace it, because a worn rest can lead to uneven grinding. Sump screens, too—if your grinder has a filter screen in the coolant sump, pull it out, scrub it with degreaser, and rinse it. A clogged sump screen makes coolant spray uneven, which burns the edge of your workpiece.
Once you’ve cleaned everything, let’s talk about the finishing steps that make the routine last longer. After you’ve wiped all surfaces, spray a thin coat of rust-inhibiting oil (made for hydraulic machines, not general-purpose oil) on the table, ram, and any metal surfaces that aren’t moving. I always tell customers to do this even if their shop is air-conditioned—humidity and metal create rust faster than you think. Then, run the machine through a full cycle: move the ram up and down, move the table back and forth, turn on the coolant for a minute. This distributes the oil evenly and makes sure no debris was left in the hydraulic lines. For the sump, if you drained and refilled it, run the coolant for five minutes to circulate it through the system, then check the level—you don’t want it too low, because that can suck in air and cause the hydraulic ram to jerk.
Now, how often should you do this? For shops running a hydraulic surface grinder 24/7, I recommend a daily wipe-down of the table, ram, and sump, with a deep clean (draining coolant, scrubbing T-slots, cleaning the guard, dressing the wheel) once a month. For smaller shops or hobbyists using the machine a few times a week, a deep clean every three months works. The mold shop I mentioned earlier—they started doing a monthly deep clean, and their downtime went from three days a quarter to less than two hours a month, just for routine checks. It’s a small time investment that pays off big.
I’ve also seen common mistakes that people make when cleaning their grinder. One big one: using harsh degreasers on hydraulic seals. I can’t stress this enough—seals are made of nitrile or polyurethane, and harsh chemicals break them down, leading to leaks. Another mistake: not dressing the wheel after cleaning. A clogged, glazed wheel will leave a fuzzy finish on your workpiece, and no amount of wiping the table will fix that. The third mistake: skipping rust prevention. I had a customer once who forgot to oil the table after cleaning, and within a week, a tiny rust spot had scratched a $5,000 mold plate they were grinding. That’s a mistake no one wants to make.
If you’re still learning how to care for your hydraulic surface grinder, let me tell you: cleaning isn’t just a chore, it’s how you protect your investment. A good grinder from a reputable supplier will last 15 years or more with proper maintenance, but neglect the cleaning, and you’ll be replacing hydraulic seals, fixing stuck rams, and dealing with inconsistent parts long before you should. At the end of the day, a clean grinder gives you consistent results, less downtime, and a safer working environment.

If you’re looking for a reliable hydraulic surface grinder, or you need help setting up a maintenance routine that works for your shop, reach out to our team to discuss your needs. We’re here to make sure your machining equipment runs as well as it can, because your success is our success.
Horizontal Surface Grinder References
Surface Grinder Maintenance and Safety Guidelines, National Institute for Occupational Safety and Health
Hydraulic System Sealing and Care for Machine Tools, Society of Manufacturing Engineers
Precision Machining Equipment Maintenance, American Machinist Handbook
Wuxi Mingxu Machinery Equipment Co., Ltd.
As one of the most professional hydraulic surface grinder manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy the best hydraulic surface grinder for sale here from our factory. Also, custom service is available.
Address: No. 5-5 Jinke Wealth Plaza, Changjiang North Road, Xinwu District, Wuxi City, Jiangsu Province
E-mail: yingyingmxjd@163.com
WebSite: https://www.mingxu-china.com/
