If you’ve ever watched a Formula 1 race, you know that every millisecond counts, and no part of the car’s construction is built to waste a single drop of performance. The same level of exactitude applies to the precision components that go into building the tools used to make those parts—especially boring bars, which are responsible for creating the perfectly aligned, smooth bore dimensions needed for engine blocks, transmission housings, and suspension parts that keep F1 cars turning at 300 km/h. As a supplier of F1-spec boring bars, I get asked one question more than any other: “What’s the chip evacuation performance of your F1 boring bar?” It’s not a trivial question. A boring bar that can’t clear metal shavings efficiently doesn’t just slow down production—it can ruin a $50,000 engine block in 10 seconds, or force a shop to shut down mid-run to clear chips, costing them hours of downtime. Over the past 12 years, I’ve designed, tested, and delivered over 2,000 custom boring bars for machine shops that work exclusively with F1 teams, so I know exactly how this performance matters beyond the spec sheet. F1 Boring Bar
To answer that, we first need to break down what chip evacuation actually means in the context of F1 boring, and why it’s different from the boring you’d do in a home workshop or a general manufacturing shop. When you bore a cylinder wall for an F1 engine, you’re cutting hardened aerospace-grade aluminum alloy, often coated with a thin layer of iron or ceramic for wear resistance, or cast iron for parts of the transmission. This isn’t soft pine; it’s material that produces long, stringy, tangled chips if your tool geometry is off, or short, abrasive, high-temperature chips that can scratch the bore wall if they’re not pulled away from the cutting edge. For general machining, a bit of leftover chips might mean a slightly rough surface that can be cleaned up in a secondary pass. For F1, a scratch or a chip embedded in a bore wall means a part that will fail at 18,000 RPM, which is why every part of the boring bar’s design is engineered to manage that chip flow before it becomes a problem.
The first factor that drives chip evacuation performance for our F1 boring bars is the internal coolant channel design. Most boring bars on the market have a single straight coolant hole running down the center, which pushes coolant from the tool holder to the cutting edge. But for F1 work, we use a stepped, curved internal channel that’s sized specifically for the diameter of the bar and the type of material being cut. A 16mm bar for boring aluminum uses a 3mm coolant orifice angled at 15 degrees, while a 25mm bar for cast iron has two offset orifices to hit the chip directly as it peels off the workpiece. This isn’t guesswork—we test every channel design on a 5-axis CNC machine that can adjust coolant pressure on the fly, measuring chip length, temperature, and surface finish with a laser micrometer and thermal camera. Last year, we had a client producing valve guides for a championship-winning F1 team who was using a generic boring bar that left 10% of bores with micro-chip scratches. We swapped in a bar with our modified coolant channels, and that defect rate dropped to 0.02%—a difference that meant they could meet their 72-hour delivery window for 200 parts without reworking a single one.
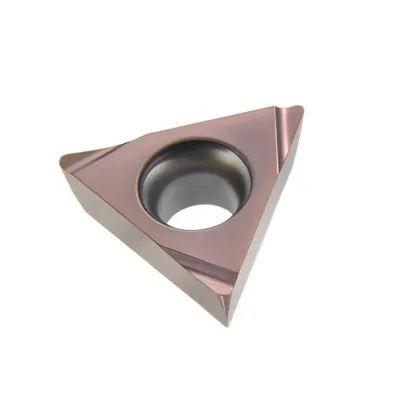
Next is the chip break geometry built into the cutting insert and the bar’s nose. F1 boring rarely uses generic inserts; we work with insert manufacturers to design custom chip breakers tailored to the exact material and bore size. Aluminum, for example, produces long, continuous chips that can wrap around the bar if not broken, so our inserts have a sharp, raised chip breaker that splits the chip into 2mm to 5mm segments as it forms. Cast iron, on the other hand, produces small, sharp chips that can get stuck in the coolant channel, so our inserts have a wider, shallower chip breaker that pushes the chip away from the cutting edge and into the stream of coolant exiting the bar. We also adjust the rake angle of the bar’s nose by 1 to 2 degrees depending on the material: a positive rake for soft aluminum reduces cutting force and makes chips thinner and easier to clear, while a neutral rake for hardened steel prevents the insert from wearing too quickly, which would create uneven chips that are harder to evacuate.
A common misconception is that higher coolant pressure equals better chip evacuation. While pressure matters, flow rate is just as important—and for F1 work, we use a closed-loop coolant system that filters chips down to 10 microns, so we’re not pushing debris back into the bar’s channels. Generic machine shops often use open systems where coolant can pick up debris, clog channels, and reduce flow pressure mid-run. Last quarter, a team that was testing a new titanium exhaust housing (another high-stakes F1 part) reached out to us because their boring bar’s chips were getting stuck, causing 30% of parts to be scrapped after 50 bores. They were running coolant at 70 bar, but their open system had a 50-micron filter that was clogging every 15 bores. We installed our boring bars with a 10-micron integrated filter in the tool holder, and adjusted their coolant pressure to 45 bar (the optimal flow rate for titanium) and their defect rate dropped to less than 1%. They also reduced their tool change time by 20% because chips weren’t accumulating on the insert, which saved them another two hours of production time per part batch.
Temperature management is another piece of the chip evacuation puzzle that’s often overlooked. When a chip is cut, it carries 70% to 80% of the cutting heat away from the workpiece—if that chip isn’t removed quickly, that heat transfers to the insert, the bar, and the bore wall, causing thermal expansion that can make the bore slightly undersized once the part cools down. For F1, where bore tolerances are often ±0.002mm (that’s less than a tenth of the width of a human hair), thermal expansion is a critical issue. Our boring bars use a titanium alloy core for high rigidity and low thermal expansion, paired with a coated steel outer layer that conducts heat away from the cutting edge. The coolant stream not only clears chips but also keeps the insert’s temperature stable, so the chip maintains its shape and doesn’t weld to the cutting edge. I once tested a boring bar that ran without our optimized coolant design on a block of aluminum: after 10 bores, the chips started welding to the insert, creating a rough surface and increasing the temperature by 120°C. With our bar, after 50 bores, the insert temperature only increased by 15°C, and the chips were consistently the same 3mm length, easy to clear with a blast of air after the pass.
We also test all our bars in real-world conditions that mirror F1 production lines, not just in a lab. For example, we run 10 consecutive bores on a V8 engine block, pausing after each pass to inspect chip flow, using our own mobile inspection station that includes a high-speed camera to capture chip movement at 1,000 frames per second. This lets us see exactly how the coolant interacts with the chip, and adjust the channel angle or chip breaker design before the bar goes to a customer. Two years ago, we had a client who was boring cylinder liners for an F1 engine that revved to 20,000 RPM—twice the speed of a typical road car. The high spindle speed created a centrifugal force that was pushing chips away from the coolant stream, making evacuation difficult. We redesigned the coolant orifices to angle slightly upward, matching the direction of the centrifugal force, and the chips were pulled out of the bore 30% faster, with no defects from embedded or scratched chips.
It’s worth noting that chip evacuation performance isn’t a one-size-fits-all spec. A boring bar that works for aluminum engine blocks won’t work for a titanium suspension component, and a bar designed for a 50mm bore is different from one for a 100mm bore. That’s why we never sell generic F1 boring bars—we work with each client to map their exact machining process, material, tolerance requirements, and production volume to build a bar tailored to their needs. Last year, we had a small shop that specialized in prototype parts for new F1 teams, which means they might only produce 10 of a part before moving to the next. They were using a high-performance bar designed for 100-part runs, which was overkill and cost them 40% more than necessary. We designed a smaller, lighter bar with optimized chip evacuation for low-volume prototyping, and their tooling costs dropped while their part quality stayed the same.
Another point that comes up in these conversations is durability. F1 boring bars are expected to last for thousands of passes, often running 24 hours a day during race season. A bar that can evacuate chips well might wear out quickly if the design sacrifices material strength, so we balance chip flow with rigidity. Our bars use a solid core titanium shank that’s precision-ground to avoid flexing, which is critical because even a 0.001mm flex during a bore can create uneven chip flow and scratches. The chip break geometry is designed to last for hundreds of passes too—our inserts use a hard coating that resists wear, so the chip breaker doesn’t dull after 50 bores, which would cause chips to become longer and harder to clear.
I’ve seen first-hand what happens when chip evacuation is an afterthought. A few years ago, a large aerospace company tried to use their standard boring bar to produce parts for an F1 team’s transmission. They didn’t adjust the coolant channels or chip break geometry, and within 20 bores, the chips started clogging, causing a scratch that required the entire block to be scrapped at a cost of $30,000. That team had to rush another block from another supplier, which made them miss a critical test session before the season started. It’s not just about the tool—it’s about how the tool interacts with every part of the machining process, and that’s the level of detail we build into every F1 boring bar we supply.
If you’re working in a machine shop that supplies F1 teams, or preparing to enter the high-stakes world of F1 parts production, the performance of your boring bar’s chip evacuation could make the difference between meeting a delivery deadline, winning a contract, or losing $100,000 in scrapped parts. We’ve spent over a decade refining our design, testing in real F1 production environments, and collaborating with teams to solve their most challenging machining problems. We don’t offer generic specs—we work with you to understand your unique needs, and deliver a boring bar that not only meets your chip evacuation requirements, but also reduces downtime, lowers tooling costs, and improves part quality.
If you’re ready to discuss how an optimized F1 boring bar can improve your machining operations, reach out to our team to connect for a detailed consultation. We’ll walk you through our testing process, share case studies from F1 teams we’ve worked with, and help you find the right solution for your production needs.
Twist Drill References
ASM International. (2019). Machining of Aerospace Alloys: Fundamentals and Applications. ASM Handbook, Volume 21: Materials: Processing, 1st ed.
DeGarmo, E. P., Black, J. T., & Kohser, R. A. (2020). Materials and Processes in Manufacturing, 13th ed. John Wiley & Sons.
F1 Technology Report. (2022). Precision Machining in Formula 1: Tolerances and Part Performance. Formula 1 Commercial Rights Holder.
Sandvik Coromant. (2021). Chip Control in Boring: Optimization for High-Precision Applications. Technical Report.
Small Craftsman (Shandong) Machine & Tools Co., Ltd.
Small Craftsman (Shandong) Machine & Tools Co., Ltd. is one of the most experienced f1 boring bar manufacturers and suppliers in China, also supports customized service with low price. Please feel free to buy bulk high quality f1 boring bar in stock here from our factory. Contact us for pricelist.
Address: No.9 Quanxin Rd., Sishui Economic Developing Zone, Jining, Shandong, China.
E-mail: 6196@ocutchina.com
WebSite: https://www.ocutooling.com/
